Product Specifications
|
Parameter |
Value |
|
Dimensional Tolerance (<500mm) |
Tolerance ≤±0.01mm, Center distance ≤±0.01mm |
|
Dimensional Tolerance (>500mm) |
Tolerance ≤±0.02mm, Center distance ≤±0.02mm |
|
Surface Roughness (Fit surfaces) |
Ra≤1.6μm |
|
Surface Roughness (General surfaces) |
Ra≤3.2μm |
|
Surface Finish |
Burrs removed, sharp edges broken, thread holes chamfered, cleaned and washed |
|
Process Route |
Hot forging + CNC precision machining |
|
Heat Treatment |
Annealing, normalizing, quenching & tempering (as agreed) |
|
Typical Applications |
High-precision transmission forgings, precision hydraulic valve body blanks, precision equipment load parts |
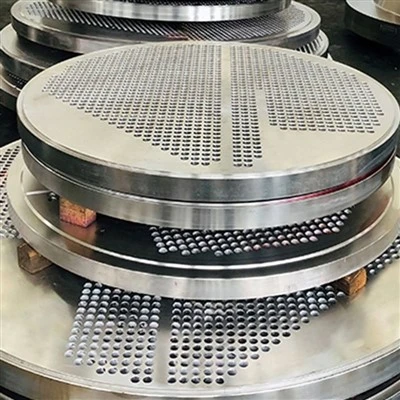
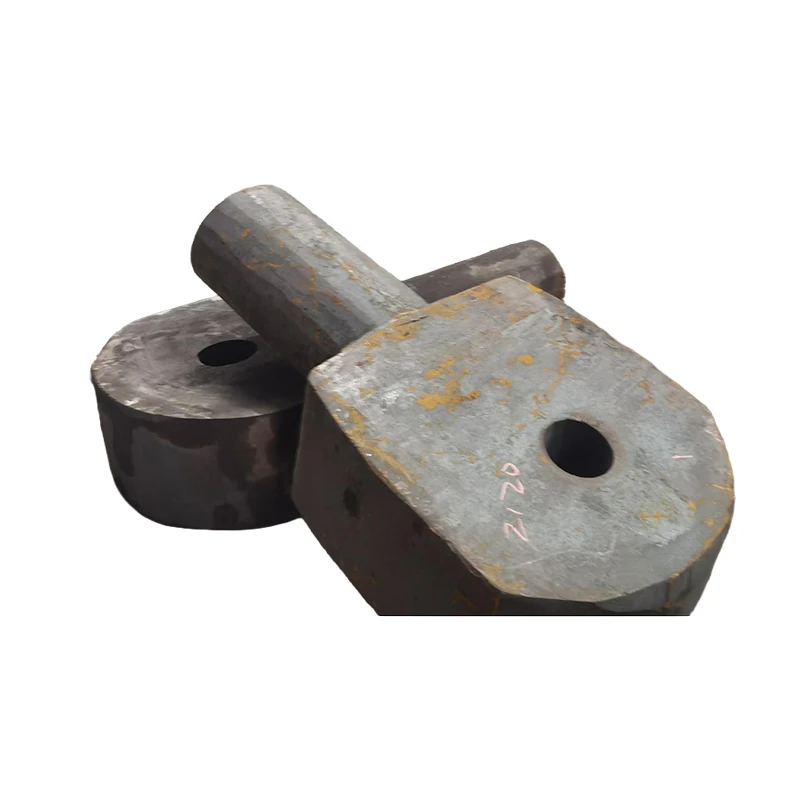
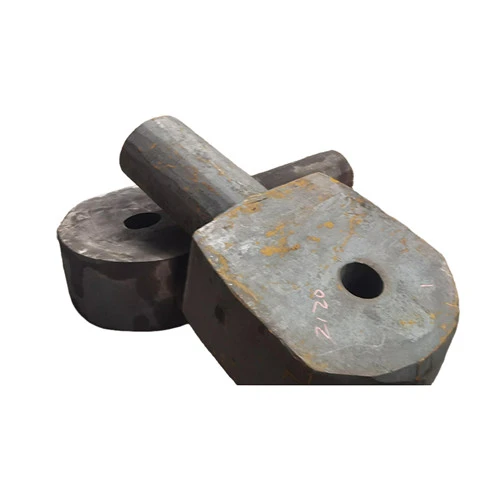
Hot Forging with Precision Machining Combined
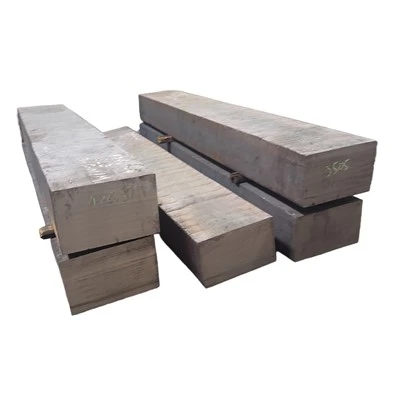
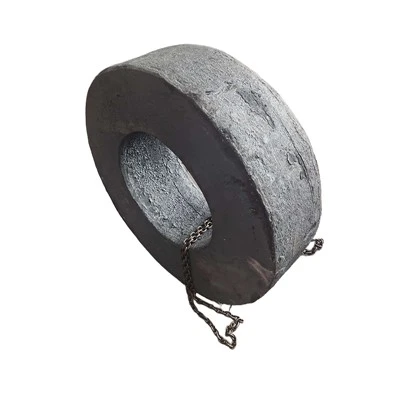
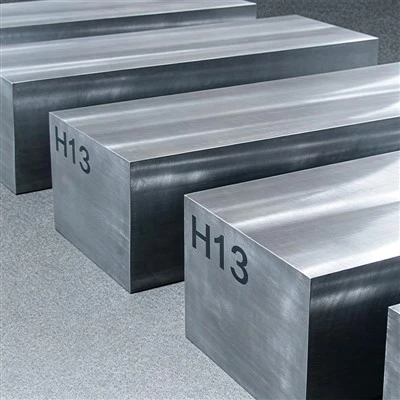
Hot metal forging is our core capability. But we do more than just produce hot forged blanks. We also do precision machining on the forged parts. This means we can deliver parts that are ready for assembly. You do not need to send the blank to another shop for finishing. We have 3000-ton forging presses for the hot forging step. We have CNC machine tools for the finishing step. This combination of capabilities sets us apart from shops that only provide rough forgings.
-
Tight Dimensional Accuracy After Machining
For parts under 500 millimeters, we hold the dimensional tolerance to plus or minus 0.01 millimeters. The center distance tolerance is also plus or minus 0.01 millimeters. For parts over 500 millimeters, the dimensional tolerance is plus or minus 0.02 millimeters. The center distance tolerance is also plus or minus 0.02 millimeters. These numbers are achievable because we control the forging quality and the machining quality in one facility. The fit surfaces have a surface roughness of Ra 1.6 micrometers or less. The general machined surfaces are held to Ra 3.2 micrometers or less.
-
Surface Finish and Cleanliness
We remove all burrs and break sharp edges. Thread holes are chamfered at the opening. The parts are cleaned and washed. There are no scratches or metal chips remaining on the parts. This level of finish is important for parts that go directly into assembly. You should be able to install the part without any cleaning or deburring. Our process includes a final cleaning step for every part.
Equipment and Process Control
Our hot forging equipment includes a 3000-ton press. This gives us the force needed to form large blanks and to refine the internal grain structure. After forging, we do heat treatment in our own car-bottom resistance furnace. This removes internal stress and improves machinability. Our machining shop has CNC lathes, CNC gantry mills, and vertical boring and milling centers. We can do turning, milling, boring, drilling, and tapping all in-house. For inspection, we have a spectrometer, universal testing machine, impact tester, and Leeb hardness tester.
Hot Tags: hot metal forging, China hot metal forging manufacturers, suppliers, factory