
Product Specifications
|
Parameter |
Value |
|
Dimensional Tolerance (<500mm) |
Tolerance ≤±0.02mm, Center distance ≤±0.02mm |
|
Dimensional Tolerance (>500mm) |
Tolerance ≤±0.04mm, Center distance ≤±0.04mm |
|
Surface Roughness (Fit surfaces / Bearing bores) |
Ra≤1.6μm |
|
Surface Roughness (General surfaces) |
Ra≤3.2μm |
|
Surface Finish |
Burrs removed, sharp edges broken, thread holes chamfered, cavities cleaned |
|
Machinable Materials |
Gray cast iron, ductile iron, aluminum alloy, cast steel |
|
Machining Focus |
Bearing bore positions, center distances, mounting surfaces |
|
Typical Applications |
Reducer housings, gearbox housings, transmission housings |
Precision Gearbox Housing Machining
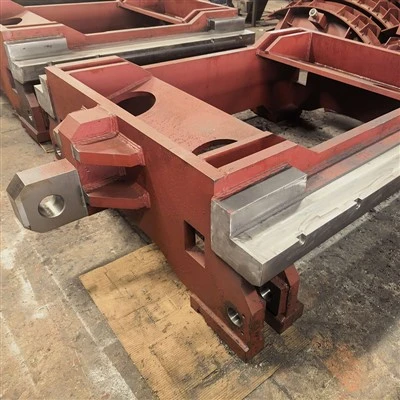
We specialize in reducer housing processing. The most critical features of a reducer housing are the bearing bore positions and center distances. These directly affect the gear meshing quality. If the center distance is off, the gears will not mesh properly. This causes noise, rapid wear, and short service life. We treat center distance accuracy as our primary control target. We have experience with worm gear reducers, planetary reducers, and gear reducers. Our machining process ensures the housing supports the gears correctly.
-
Accurate Bearing Bores and Center Distances
The dimensional tolerance for reducer housings under 500 millimeters is plus or minus 0.02 millimeters. The center distance tolerance is also plus or minus 0.02 millimeters. For housings over 500 millimeters, the tolerance is plus or minus 0.04 millimeters. The center distance tolerance is also plus or minus 0.04 millimeters. The bearing mounting surfaces have a roughness of Ra 1.6 micrometers or less. The general machined surfaces are held to Ra 3.2 micrometers or less. We remove all burrs and break sharp edges. Thread holes are chamfered. The parts are cleaned and washed.
-
Clean Internal Cavities
Reducer housings have internal cavities that hold the gears and bearings. Metal chips from machining can collect inside these cavities. Leftover chips can damage the gears or bearings when the reducer runs. We clean the cavities thoroughly after machining. We inspect to make sure all chips are removed. This simple step prevents costly failures. We treat it as a standard part of our process.
Cast and Machined in One Facility
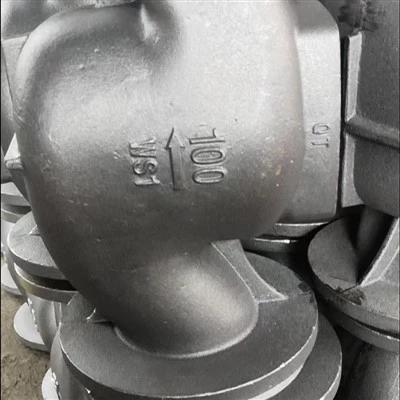
We have our own casting shop. We produce gray cast iron, ductile iron, and aluminum alloy reducer housing blanks. This means we can offer a complete service. We cast the blank and machine it to the finished dimensions. You do not need to source the blank separately. You do not need to coordinate between a foundry and a machine shop. This reduces your supply chain risk and saves your time. We inspect every batch before shipping and keep photo records.
Hot Tags: reducer housing processing, China reducer housing processing manufacturers, suppliers, factory